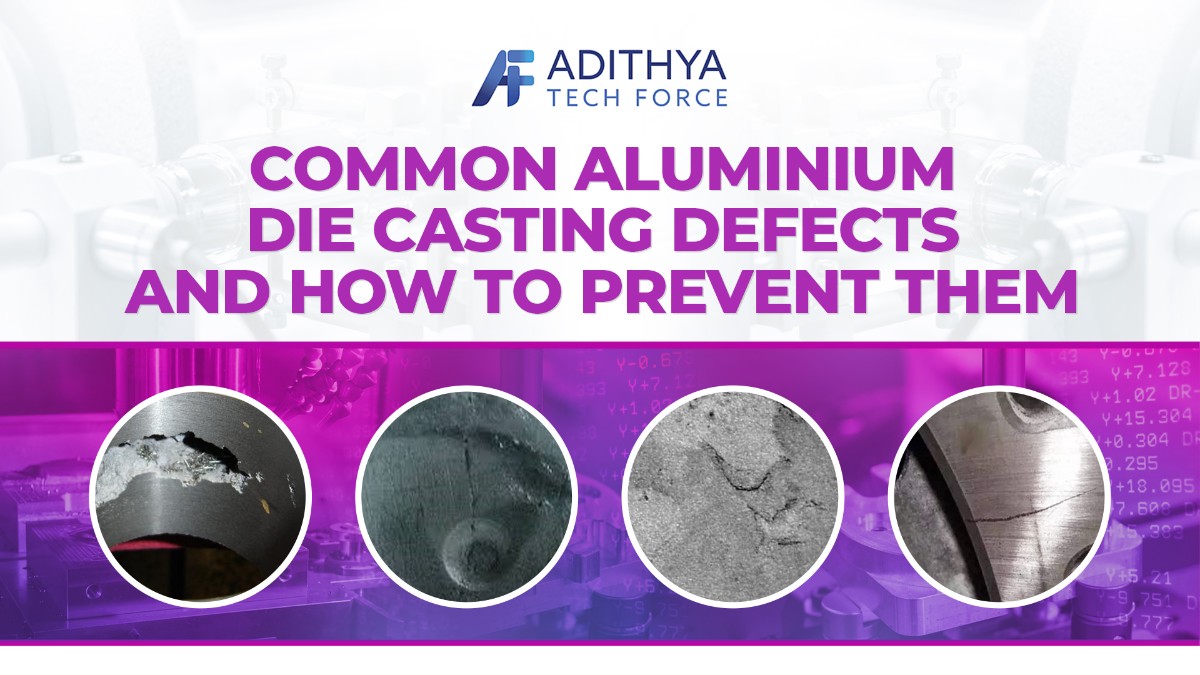
Aluminium die casting is one of the most critical manufacturing processes in the aerospace, automotive and consumer electronics sectors with high precision and efficiency. However, as much as the process is useful, it is susceptible to a range of aluminium die casting defects that could invalidate the quality and performance of the end products. Awareness of these defects and preventive action is important for the manufacturers to consider, particularly in countries like India, where the aluminium die casting industry is growing at a fast rate.
Aluminium Die Casting Defects and How to Treat Them
Quick Reference Diagnostic Table
| Visual Symptom | Defect Name | Primary Cause | Quick Fix / Next Step |
| Blisters or smooth, round holes | Gas Porosity | Trapped air or hydrogen gas | Audit venting system; rotary degas melt. |
| Spongy, jagged cavities in thick walls | Shrinkage | Volume loss during cooling | Increase intensification pressure; check cooling lines. |
| Overlapping lines or incomplete fill | Cold Shuts / Misruns | Low temperature or slow injection | Increase die/melt temp; boost injection speed. |
| Thin metal fins at the parting line | Flash | Insufficient clamping force | Verify machine tonnage; clean die faces. |
| Jagged tearing after ejection | Hot Cracks | Thermal stress / uneven cooling | Balance cooling channels; increase corner radii. |
1. Porosity and Air Entrapment
Porosity is in the form of minute cavities or voids within the casting, primarily due to gas entrapment or shrinkage on solidification. Aluminium die casting porosity may be caused by dissolved hydrogen in the molten metal or due to poor venting leading to air entrapment on injection. Aluminium casting voids can reduce the mechanical strength of the casting considerably and affect pressure tightness.
Prevention Strategies:
- Melt Treatment: Rotary degassing techniques employing inert gases like nitrogen can degas dissolved hydrogen from molten aluminium efficiently and thus reduce gas porosity accordingly.
- Optimized Gating and Venting: Optimized gating system design with free flow bias of metal and use of adequate vents will decrease turbulence and provide an opportunity for escape of trapped air while casting.
2. Shrinkage and Microporosity
Shrinkage porosity has been discovered to have developed since the liquid metal is not sufficient to make up for volume loss during solidifying and form voids either in the solidification front or at the surface. Microporosity is very small, typically micro-sized pores which have developed because of rapid rates of cooling and low volumes of feeding molten metal.
Prevention Strategies:
- Proper Gating Design: Ensuring that the gating system allows proper feeding of molten metal during solidification can counteract shrinkage.
- Controlled Cooling Rates: Control of cooling rates by proper die temperature and application of chills can ensure uniform solidification, avoiding the possibility of microporosity.
3. Cold Shuts and Misruns
Cold shuts are the result of two streams of molten metal not fusing together well and giving a poor seam. Misruns are the result of the molten metal not fully filling the mould cavity, leading to short castings. Both of these aluminium die casting defects are usually caused by low pouring temperatures, low injection rates or complex mould designs.
Prevention Strategies:
- Optimal Pouring Temperature: Keeping the optimum pouring temperature will cause the molten metal liquid to reach the brim of the mold.
- Enhanced Mold Design: Decrease in mold geometry and effective venting can improve metal flow and reduce opportunities for cold shuts and misruns.
4. Flash and Flash Lines
Flash refers to excess metal that escapes between the halves of the mould, freezing into thin extensions at the parting line. Flash lines are residual ridges that can result in dimensional accuracy and appearance defects in castings.
Prevention Strategies:
- Die Maintenance: Regular maintenance and inspection of dies ensures that there is proper alignment and surface integrity to prevent metal leakage.
- Controlled Injection Parameters: Adjusting injection pressures and making sure of adequate clamping force can help in minimizing the occurrence of flash.
5. Hot Cracks and Tears
Hot cracks, otherwise referred to as hot tears are solidification cracks in the casting due to thermal stresses. Most of the aluminium die casting defects result from some restrictions that will inhibit the free contraction of the metal when cooling and thus stress build-up.
Prevention Strategies:
Uniform Cooling: Scheduling the mold to make sure uniform cooling and solidification can help in minimising thermal gradients responsible for inducing stress.
Alloy Selection: Employing alloys with appropriate composition and grain structure can drastically improve the hot cracking resistance of the casting.
ALSO CHECK – Top Aluminium Alloy Casting Grades and Their Uses
Aluminium Die Casting in India: Challenges and Solutions
Indian aluminium casting sector has seen significant growth on the back of rapidly growing automotive and consumer electronics industries. Processors do have specific issues, however, such as sustaining quality levels against high volume of production and containing costs.
Strategies for Indian Manufacturers:
- Investment in Technology: Next-generation technologies would be installed in casting and simulation software that would help anticipate and avoid defects in aluminium die casting to provide a product quality of higher standard.
- Skilled Workforce Development: Training employees in best practices in the operation of die casting ensures process control and defect prevention.
Adithya Tech Force India’s Role in Enhancing Quality Standards
Adithya Tech Force India is today an excellence-oriented company of the highest merit in the aluminium casting business. With door-to-door solutions comprising design, manufacture, and quality control, high-end companies for aluminium die casting in India such as Adithya Tech Force India assist producers to obtain flawless castings. Its contributions include:
- Quality Control Measures: Implementing stringent inspection protocols and sophisticated testing equipment to detect and rectify aluminium die casting defects early during the production stage.
- Process Optimization: Working with customers to optimize casting operations, streamline mold designs, and choose suitable materials to reduce the occurrence of defects.
Final Thought
To conclude, for Indian manufacturers, maintaining contact with current technology and the adoption of strict quality control procedures is required to be competitive internationally. Collaborations with industry players such as Adithya Tech Force India can similarly continue to increase capacity, which ensures the delivery of high-quality, fault-free best aluminium die castings.
Frequently Asked Questions (FAQs)
- What causes gas porosity in aluminium die casting?
Gas porosity is primarily caused by air trapped in the die cavity during high-speed injection, vaporized die release agents or dissolved hydrogen present in the molten aluminium before it is poured. - How can cold shuts and misruns be prevented?
Cold shuts and misruns can be prevented by increasing the die and pouring temperatures, boosting the injection speed and improving the venting and gating design so the molten metal can completely fill the cavity before solidifying. - Why does flash occur in high-pressure die casting?
Flash occurs when molten metal escapes along the parting line of the mould. This happens when the injection pressure exceeds the clamping force (tonnage) of the machine or if the die faces are worn, damaged or misaligned.